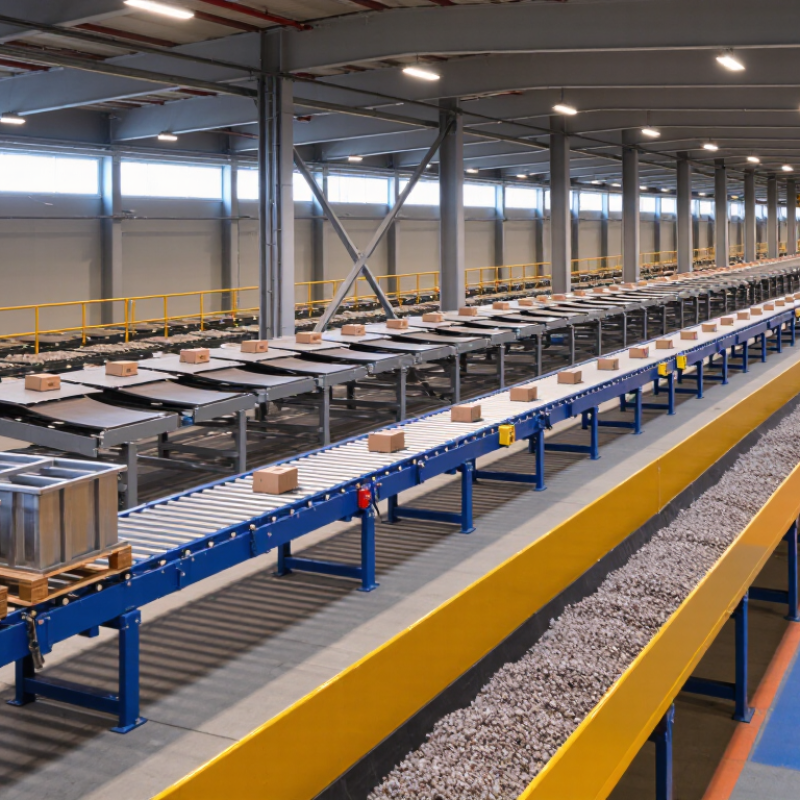
2026 Top Industrial Chain Conveyor Types for Global Buyers
In 2026, global buyers need conveyor choices that match real production conditions, not attractive catalog claims. An Industrial Chain Conveyor can move heavy loads through demanding industrial environments. However, chain strength alone does not determine system performance. Layout, load shape, speed, temperature, cleaning routines, and maintenance access matter equally. This guide examines leading industrial chain conveyor types for international purchasing decisions. It connects technical design with practical factory experience. Real projects often reveal the difference.
The comparison covers roller chain conveyors, slat chain conveyors, drag chain conveyors, apron conveyors, and bucket chain systems. Each design handles specific materials, routes, and operating pressures. Roller chains may suit pallets and rigid loads. Slat chains can support controlled product flow across processing lines. Drag and apron systems often manage bulk materials under harsh conditions. Bucket conveyors can lift granular products while limiting floor space. Buyers should verify load capacity, chain pitch, drive configuration, corrosion resistance, guarding, and spare-part availability. Safety compliance and supplier documentation also deserve close review. Ask for drawings, test records, maintenance schedules, and references from comparable facilities. Not every supplier presents this information clearly. That is a warning sign.
A perfect conveyor does not exist. Selection always involves compromise. A lower purchase price may create higher cleaning or downtime costs. A stronger chain may add unnecessary weight and energy demand. This article therefore balances performance, reliability, service support, and total ownership cost. Some recommendations may require adjustment after site inspection. That is normal. Careful evaluation remains the safer path for global buyers.
What Industrial Chain Conveyors Are and How They Work
Industrial chain conveyors move heavy products through factories, warehouses, and assembly areas. They use one or more endless chains driven by sprockets. A motor and gearbox turn the drive sprocket, pulling the chain along a guided path. Products sit directly on the chain, rollers, slats, or pallets.
Common designs include roller chain conveyors, slat chain conveyors, drag conveyors, and pallet conveyors. Roller chains suit pallets and rigid loads. Slat conveyors handle containers with stable, continuous support. Drag conveyors move bulk materials inside enclosed channels. Pallet systems support accurate assembly and transfer work. The right type depends on load weight, surface condition, speed, incline, and required spacing.
A typical system includes a drive unit, return rail, tensioning device, guards, and sensors.
Operators should check chain alignment and lubrication regularly. Small alignment errors can create noise, uneven wear, or sudden stoppage. Heavy loads need stronger frames and carefully selected sprockets. Wet or dusty areas may require corrosion-resistant parts and sealed bearings.
A frequent planning mistake is choosing capacity from weight alone.
Load shape matters. A narrow pallet may twist, while a soft package may need full support. Conveyor speed also affects product stability. Higher speed is not always better. Factory trials can reveal problems that drawings miss, especially at transfers and curves. Safety guarding and emergency stops must match local workplace requirements.
Main Industrial Chain Conveyor Types and Their Structures
Industrial chain conveyors use linked metal components to move heavy, hot, or irregular loads. Their basic structure includes chains, sprockets, a support frame, guides, shafts, bearings, and a drive unit. The chain carries the product, while the sprockets control its movement. A well-aligned frame reduces vibration and uneven wear.
Drag chain conveyors use one or more chains with flights inside an enclosed trough. They suit bulk materials such as pellets, ash, and wood chips.
Apron conveyors use overlapping metal pans fixed to chains. Their rigid surface handles sharp parts, castings, and high-temperature products.
Slat chain conveyors use connected plates, often with a smoother surface for cartons, containers, and assembly work.
Bucket chain conveyors attach buckets to links and lift granular materials vertically.
Structure decides maintenance effort. Open frames allow quick inspection but expose chains to dust and moisture. Enclosed frames offer better protection, yet they can hide early wear.
In plant inspections, I check sprocket tooth condition, chain stretch, return-rail contact, and lubrication points. Small alignment errors can create loud impacts and premature failure. They are easy to miss.
Buyers should compare load weight, conveyor length, inclination, speed, product temperature, and cleaning needs. A drawing may look correct but still ignore access for repairs. That oversight deserves a second review before production.
Key Performance Factors for Global Conveyor Selection
Industrial chain conveyors remain essential for moving pallets, bins, steel parts, and heavy assemblies in 2026. Global buyers should evaluate performance before comparing prices. A drag chain conveyor suits dense loads and controlled production lines. A slat chain conveyor handles products needing stable, continuous support. Overhead chain systems save floor space, but installation access can become difficult.
Load weight matters first. Check both average and peak loads. A conveyor carrying 300 kilograms occasionally may need a higher-rated drive. Measure chain speed, pitch, transfer spacing, and daily operating hours. Motor efficiency affects long-term costs. Harsh dust, moisture, heat, and cleaning chemicals also influence material selection. Stainless components may resist corrosion better, but they can increase initial investment. Noise is another practical factor. Workers notice it quickly.
Tips: Request a load profile, not only a maximum weight. Test the smallest product and the heaviest pallet. Confirm emergency stops, guarding, and maintenance access. Ask for spare-chain availability and documented service procedures. These details often matter more than polished specifications.
In real projects, layout changes create unexpected stress. I have seen a suitable conveyor fail because operators added uneven loads later. That experience supports modular designs and adjustable guides. No selection is perfect. Buyers should leave room for future speed, width, and capacity changes. A site trial can reveal transfer jams that drawings miss. Measure those results before approving final production.
2026 Top Industrial Chain Conveyor Types for Global Buyers - Key Performance Factors for Global Conveyor Selection
| Conveyor Type | Typical Load / Material | Typical Speed Range | Typical Incline Capability | Operating Temperature Guidance | Key Performance Factors | Main Advantages | Common Limitations | Typical Applications | Selection Priority |
|---|---|---|---|---|---|---|---|---|---|
| Roller Chain Conveyor | Pallets, crates, bins and heavy unit loads; approximately 50–2,000 kg per load depending on frame and chain design. | 0.05–0.5 m/s for controlled heavy-load handling. | Generally horizontal; inclines commonly limited to about 5°–10° without special load-retention measures. | About −20°C to 80°C with standard materials; higher temperatures require suitable lubricants and components. | Chain pitch, allowable chain tension, sprocket alignment, load distribution, drive torque and duty cycle. | High load capacity, positive drive, robust construction and suitability for accumulation systems. | Higher noise and maintenance than belt conveyors; exposed chain can require guarding and lubrication. | Pallet transfer, automotive components, metal fabrication and warehouse handling. | Load weight, pallet underside, accumulation pressure and required throughput. |
| Tabletop Chain Conveyor | Bottles, cans, cartons, jars and packaged products; typically light to medium loads. | 0.1–1.0 m/s; higher speeds are possible with suitable product stability and lubrication. | Usually horizontal; approximately 5°–15° with profiled or high-grip chain and proper product control. | About −10°C to 80°C for common polymer chain materials; stainless designs support more demanding sanitation environments. | Chain width, product contact area, coefficient of friction, back pressure, transfer gaps and washdown requirements. | Smooth product transfer, compact layout, easy curves and good compatibility with packaging lines. | Products may tip, slide or scratch if speed, chain surface and guide rails are incorrectly matched. | Food and beverage packaging, pharmaceuticals, personal-care products and light assembly. | Product geometry, hygiene level, container stability, line speed and accumulation behavior. |
| Slat Chain Conveyor | Rigid containers, trays, cartons and irregular packaged products; light to medium loads. | 0.05–0.6 m/s, selected according to product stability and transfer requirements. | Typically horizontal; up to approximately 20° with cleated or high-friction slats. | About −20°C to 90°C depending on stainless steel, carbon steel or polymer slat construction. | Slat width, surface friction, allowable chain tension, curve radius, product orientation and sanitation design. | Stable conveying surface, modular construction, washable options and good handling of rigid products. | Not ideal for soft or unstable products; hinge and sprocket areas need regular inspection. | Bottling, canning, food processing, carton handling and container accumulation. | Product contact material, cleanability, curve requirements and allowable back pressure. |
| Apron Chain Conveyor | Hot, sharp, abrasive or heavy bulk materials; commonly 0.5–50 tonnes per hour depending on width and design. | 0.05–0.3 m/s to reduce impact, wear and material degradation. | Normally horizontal; approximately 15°–30° with suitable flights and material characteristics. | Roughly 100°C–500°C can be achievable with heat-resistant flights, chains and bearings; engineering verification is essential. | Impact loading, abrasive wear, chain pull, flight strength, sealing, heat transfer and material bulk density. | Handles severe service, hot materials and large lumps better than many belt-based systems. | Heavy structure, high power demand, slower speed and potentially significant maintenance cost. | Cement, foundries, heat treatment, waste processing, aggregates and bulk material transfer. | Material temperature, lump size, abrasiveness, impact energy and required service life. |
| Drag Chain Conveyor | Powders, granules, chips, ash and other bulk solids; commonly 5–150 tonnes per hour depending on cross-section. | 0.1–0.8 m/s; lower speeds are preferred for abrasive or fragile materials. | Approximately 15°–30° for many materials; design depends strongly on friction and bulk density. | About −20°C to 250°C for common industrial designs; higher temperatures require specialized materials. | Chain pull, trough cross-section, fill ratio, material abrasiveness, flight clearance and dust sealing. | Enclosed conveying limits dust release and supports horizontal or mildly inclined routing. | Can cause material degradation, chain wear and increased power consumption when overloaded. | Cement, grain, biomass, minerals, chemicals and industrial by-product handling. | Bulk density, moisture, abrasiveness, dust control, capacity and cleanout access. |
| Scraper Chain Conveyor | Wet, sticky or granular materials such as sludge, screenings, ash and process residues; approximately 1–100 tonnes per hour. | 0.05–0.5 m/s. | Typically horizontal; approximately 10°–25° depending on moisture and material adhesion. | About 0°C to 100°C for common systems; corrosive or hot materials require upgraded components. | Moisture content, adhesion, corrosion resistance, scraper spacing, trough wear and cleaning provisions. | Suitable for difficult wet or sticky materials and can be enclosed to control spillage. | Wear and buildup can reduce capacity; corrosion and cleaning requirements may be substantial. | Wastewater treatment, waste-to-energy, chemical processing and wet bulk handling. | Moisture, corrosiveness, buildup tendency, sanitation access and trough wear rate. |
| Bucket Elevator Chain Conveyor | Vertically conveyed powders, granules and bulk solids; commonly 5–200 tonnes per hour depending on bucket volume and speed. | Approximately 0.5–2.5 m/s chain speed, selected according to discharge method and material properties. | Vertical lifting, commonly 10–50 m or more with properly engineered supports and tension control. | About −20°C to 200°C for typical designs; high-temperature materials require specialized buckets and chains. | Bucket fill, chain tension, head and boot alignment, discharge efficiency, material degradation and casing sealing. | Efficient vertical transport with a relatively small floor footprint. | Sensitive to misalignment, overload, boot material buildup and uneven bucket loading. | Grain, cement, fertilizer, minerals, feed and other vertically transferred bulk solids. | Lift height, capacity, material flowability, dust containment and bucket filling efficiency. |
| Overhead Power-and-Free Chain Conveyor | Hanging parts, vehicles, frames and work carriers; often 20–2,000 kg per carrier depending on track and trolley design. | 0.02–0.5 m/s, with variable-speed zones and accumulation capability. | Can route through horizontal, inclined and declined sections; slopes commonly engineered within about 15°–30°. | About −20°C to 200°C; paint ovens and other high-temperature zones require dedicated chain, trolley and lubricant selection. | Carrier load, track radius, trolley wheel load, switching accuracy, accumulation logic and thermal expansion. | Separates the drive chain from carriers, enabling accumulation, buffering and flexible process routing. | More complex controls and track layout; inspection is needed at switches, trolleys and load points. | Automotive plants, painting lines, appliance assembly and multi-stage manufacturing. | Carrier weight, route geometry, accumulation requirement, process temperature and control integration. |
| Hollow-Pin Chain Conveyor | Unit loads, fixtures and custom attachments; light to medium loads, commonly up to several hundred kilograms per carrier. | 0.05–0.5 m/s. | Horizontal and inclined layouts are possible; practical angle depends on attachment geometry and load retention. | About −20°C to 100°C for standard industrial configurations. | Attachment design, pin loading, chain articulation, carrier spacing, sprocket engagement and product orientation. | Flexible attachment options and compact integration with fixtures, tooling and indexing stations. | Improper attachment loading can increase chain bending, wear and tracking problems. | Assembly, material positioning, parts washing, test stations and custom automation. | Attachment loads, indexing accuracy, fixture design, chain articulation and maintenance access. |
Industry Applications and Material Handling Requirements
2026 Top Industrial Chain Conveyor Types for Global Buyers
Industry applications now determine conveyor selection more than simple load capacity. The IFR World Robotics 2024 report recorded 541,302 industrial robot installations in 2023, showing stronger demand for automated material movement.
Chain conveyors suit pallets, crates, and heavy components. They tolerate impact better than many belt systems.
Slat conveyors support containers with uneven bottoms. Roller conveyors fit distribution centers with stable, flat loads.
Belt conveyors remain practical for powders, parcels, and continuous production lines.
Material conditions must guide every specification. Food-processing areas need corrosion-resistant surfaces and easy cleaning. Automotive plants often require high torque, precise indexing, and heat-resistant components. Mining operations demand sealed bearings, reinforced chains, and protection from abrasive dust.
The MHI 2024 Annual Industry Report identifies automation as a major supply-chain investment priority, but automation alone cannot fix poor layout design. That mistake remains common. Buyers should check load weight, speed, duty cycle, incline angle, noise limits, and available maintenance skills before ordering.
Tips: Request test videos using your actual pallets or containers. Confirm local electrical standards and spare-part availability. Keep emergency access clear. A cheaper conveyor can become expensive when cleaning takes twice as long. Also, allow room for future sensors and controls. Not every facility needs maximum speed. Reliable flow is usually better.
2026 Buying, Compliance, and Maintenance Considerations
Industrial Chain Conveyor Types: 2026 Buying, Compliance, and Maintenance Considerations
Global buyers should match conveyor construction to the product, environment, and cleaning routine. Belt conveyors suit cartons and packaged goods. Roller conveyors handle rigid loads with stable bases. Chain conveyors tolerate heavier, hotter, or irregular items. The wrong choice creates friction, noise, and avoidable downtime. A perfect specification rarely survives the first site visit.
In 2026, procurement teams should request a documented risk assessment, guarding design, emergency-stop access, and lockout procedures. ISO 12100 supports machinery risk assessment, while ISO 13849 addresses safety-related control systems. Electrical documentation should follow applicable national requirements and IEC 60204-1 principles. European buyers should also prepare for Regulation (EU) 2023/1230, which applies from January 20, 2027. Compliance paperwork is not enough. Inspect the actual transfer points and pinch zones.
Maintenance planning deserves equal attention. The U.S. Department of Energy’s 2022 Operations and Maintenance Best Practices report indicates preventive maintenance can reduce costs by roughly 12–18% compared with reactive maintenance. Schedule belt tracking checks, chain lubrication, bearing inspections, and sensor testing. Record vibration, temperature, and motor-current trends where practical. Deloitte’s 2024 Smart Manufacturing survey reported that 86% of manufacturers view smart manufacturing as important for competitiveness. Yet sensors do not repair poor installation. I would specify accessible components, spare parts, and technician training before adding complex monitoring. A simple checklist, used consistently, may outperform an impressive dashboard.